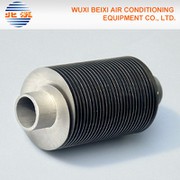
Application of Annular Finned Coil Heat Exchanger
Sep 04, 2026
Annular Finned Coil Heat Exchanger | High-Efficiency Custom HVAC & Industrial Thermal Coil
The high adaptability and efficient thermal performance ofannular finned coil heat exchangers make them widely used in commercial HVAC, industrial manufacturing, environmental protection and energy saving, refrigeration and other fields, covering most global heat exchange system scenarios. Our customized products can perfectly match different working condition requirements and are recognized by B2B customers in Europe, America, Southeast Asia, the Middle East and other regions.
1. Commercial HVAC & Central Air Conditioning System
It is the core matching component of central air conditioning, fresh air units, air handlers and fan coil units. The high-efficiency heat transfer performance ensures rapid cooling and heating of air, improves the energy-saving efficiency of air conditioning systems, and reduces equipment operating energy consumption. The compact structure is suitable for commercial buildings such as office buildings, shopping malls, hotels and hospitals, with stable operation and low noise, meeting the comfortable ventilation and temperature control requirements of commercial scenarios.
2. Industrial Drying & Textile Industry
Annular Finned Coil Heat Exchangers are widely used in textile drying, food drying, wood drying, chemical material drying and other equipment. The optimized fin pitch design prevents dust and fiber blockage, and the anti-corrosion and high-temperature resistant structure adapts to long-term continuous drying operation. The uniform heat transfer ensures consistent drying temperature, improves product drying quality, and solves the problems of uneven drying and low efficiency of traditional drying equipment.

3. Industrial Cooling & Ventilation System
Annular Fin Coil Heat Exchangers are suitable for factory workshop cooling, industrial equipment heat dissipation, mechanical and electrical equipment ventilation and cooling. The enhanced fluid turbulence design realizes rapid heat dissipation, effectively reduces the operating temperature of industrial equipment, avoids equipment failure caused by overheating, and extends the service life of mechanical equipment. It can adapt to high-temperature and high-load industrial working conditions and support 24-hour continuous operation.
4. Refrigeration & Cold Storage Industry

Matched with cold storage refrigeration units, low-temperature ventilation equipment and condensation systems. The high-purity copper tube has good low-temperature resistance, no brittle deformation in low-temperature environment, stable heat exchange performance, and effectively improves the refrigeration efficiency of cold storage equipment. It helps customers reduce refrigeration energy consumption and maintain stable low-temperature storage environment.
5. Environmental Protection & Waste Heat Recovery System
Finned Coil Annular Heat Exchangers are used for industrial waste gas heat recovery, waste water heat exchange and energy-saving ventilation systems. The efficient heat exchange structure can fully recover waste heat generated in industrial production, realize secondary energy utilization, reduce enterprise energy consumption and operation costs, and meet the global industrial energy-saving and emission-reduction standards.